
Different materials. Different conditions. The same need for controlled flow.
A transfer point handling iron ore faces very different conditions from one transferring coal, platinum ore or copper. Particle size, moisture, bulk density, abrasiveness and cohesiveness can all influence how material behaves as it moves through a plant.
For Mark Baller, Managing Director of Weba Chute Systems, this is why effective transfer point engineering starts with understanding the application rather than selecting a standard chute configuration.
“Bulk material handling is never just about moving material from one conveyor to another,” Baller says. “You need to understand what the material is, how it behaves, how it arrives at the transfer point and what needs to happen to it next.”
Weba Chute Systems has developed transfer point solutions for a broad range of commodities and operating environments over several decades. This experience extends across materials including coal, iron ore, manganese, platinum, copper, gold and chrome, as well as applications beyond conventional mineral processing.
While the fundamental engineering principles of trajectory, velocity, impact and friction remain important across these applications, the conditions engineers need to manage can vary considerably.
Abrasive materials, for example, place particular emphasis on controlling impact and managing wear. Wet or cohesive material can introduce different challenges, including buildup and restricted flow. Fine or dusty materials require careful consideration of turbulence and containment, while large lump sizes introduce their own impact and trajectory considerations.
“The commodity gives you part of the picture, but it does not give you the whole picture,” Baller explains. “Even two plants handling the same material can have very different transfer point requirements because the throughput, particle size distribution, moisture, belt speed, drop height and surrounding equipment are different.”
The position of the transfer point within the process also matters.
Material leaving a primary crusher may behave differently from material further downstream in the plant. A transfer feeding a screen has to consider how the material is presented to that equipment. Similarly, a transfer onto a conveyor needs to consider the direction and velocity of the incoming stream so that material can be loaded as effectively as possible.
This means that experience across different sections of a plant can be as important as experience with the commodity itself.
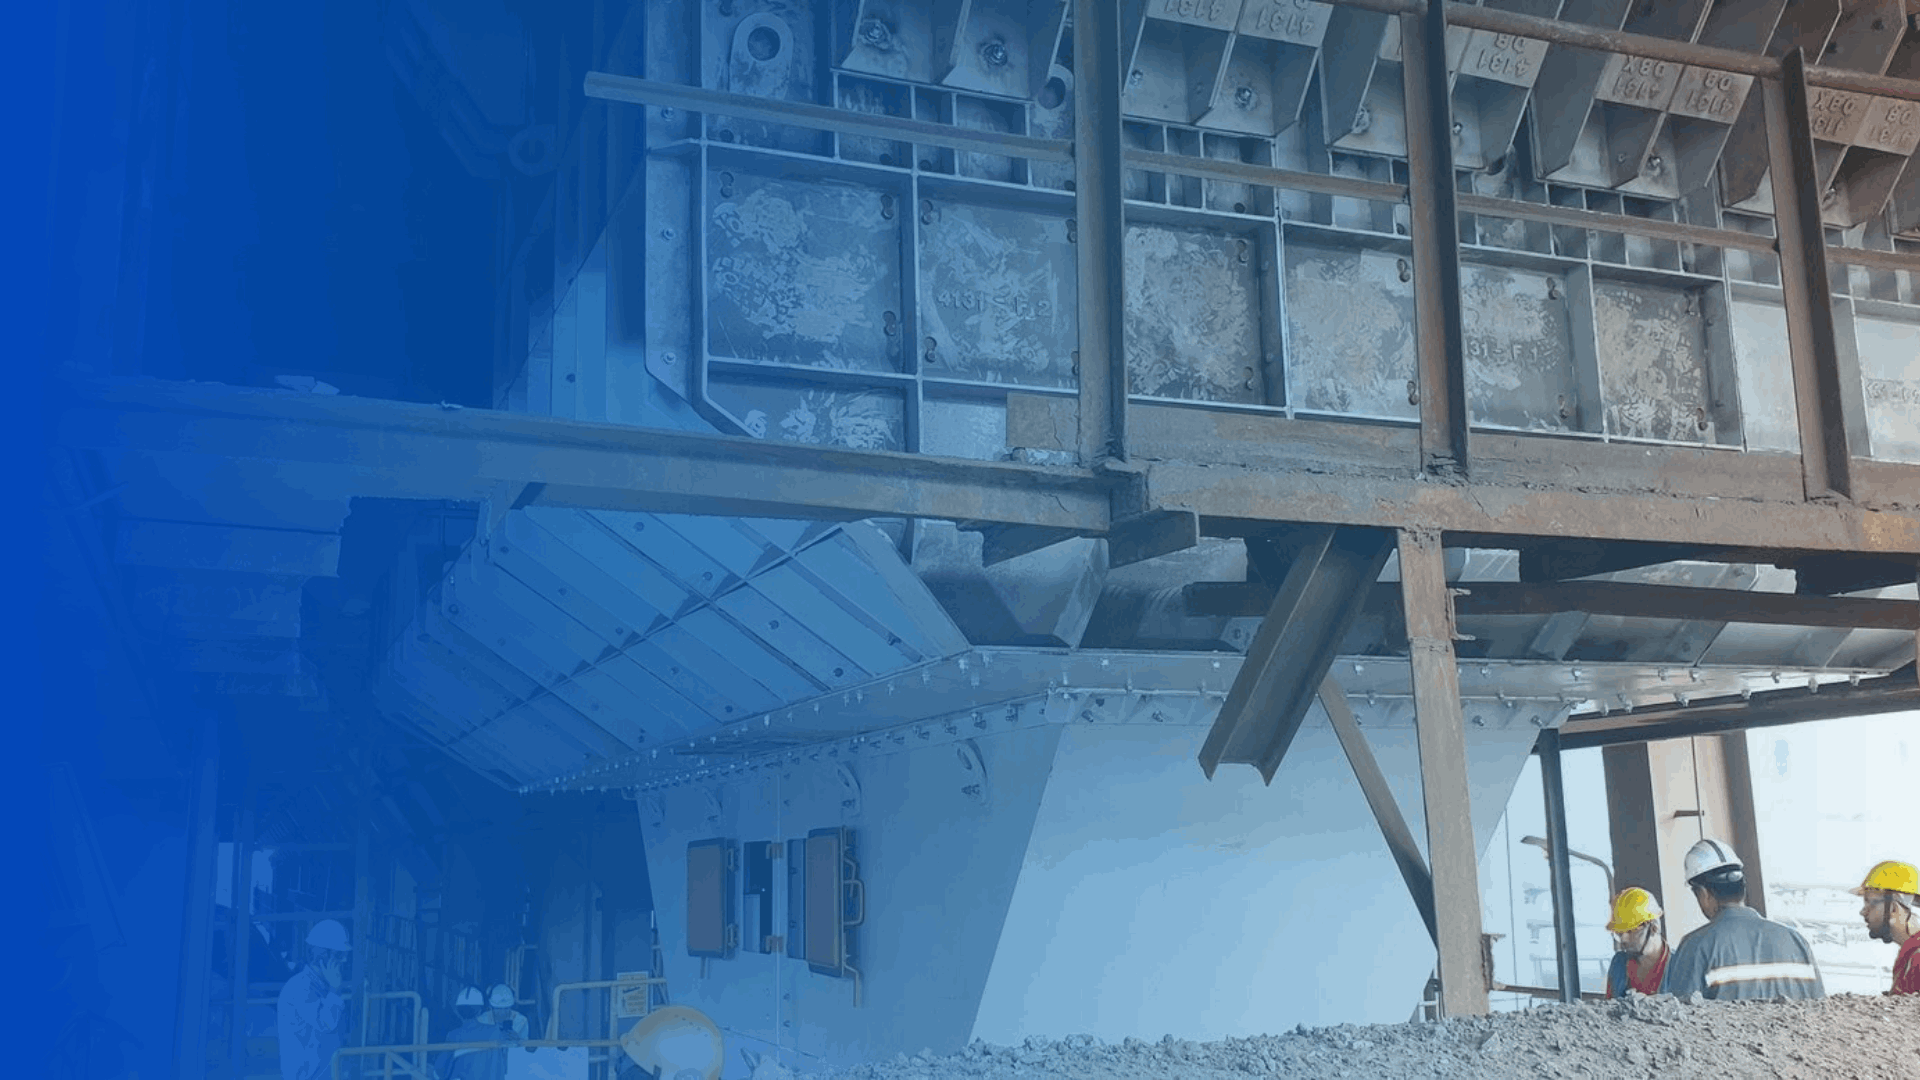
Weba engineers assess the transfer point as part of the broader materials handling system, considering the incoming and outgoing equipment as well as the behaviour of the material between them.
“When a screen, feeder, conveyor or mill is not receiving material correctly, the problem may not necessarily lie with that piece of equipment,” Baller says. “The way material is delivered to it can have a significant influence on how effectively it performs.”
Understanding these interactions becomes particularly important in existing plants, where engineers must work within established layouts and infrastructure. Conveyor positions, structural steel, available headroom, access and surrounding equipment can all influence what is practically possible.
Site information, 3D scanning and engineering data can help build an accurate picture of these conditions. Where appropriate, Discrete Element Modelling can then be used to investigate material behaviour and assess an engineering concept before fabrication.
Baller emphasises, however, that technology supports the engineering process rather than replacing the knowledge developed through practical application.
“Simulation can show us what material is doing, but engineering experience helps us understand why it is happening and what we can do about it,” he says. “That experience becomes especially valuable when you have worked with different materials, different plant layouts and different operating conditions over many years.”
The same principle extends beyond mining.
Bulk material transfer points are found in environments ranging from ports and industrial plants to other facilities where large volumes of material must be transferred reliably between equipment. Although the material and process requirements may differ, the need to understand and control the material stream remains.
For Baller, this breadth of application reinforces an important point about transfer point engineering.
“There is no universal chute that can simply be applied everywhere,” he says. “The solution has to respond to the material, the process and the plant around it.”
This is where a broad reference base becomes valuable. Experience gained across commodities and applications gives engineers a deeper understanding of the different ways bulk materials can behave, while each new transfer point is still approached according to its own operating conditions.
“The more applications you work with, the more you appreciate how important the details are,” Baller concludes. “Coal does not behave like iron ore. Manganese does not behave like platinum. Even the same commodity can behave differently from one operation to another. Good transfer point engineering starts by understanding those differences and designing around them.”